
Best overall: a stainless-rated neat cutting oil for drilling and tapping. Best for DIY general-metal work: Evodyne’s multipurpose cutting fluid, after confirming stainless compatibility. Best for sustained machine cutting: a compatible water-miscible coolant. Best for keeping lubricant on a vertical starting point: a stainless-rated cutting paste. This 2026 guide explains which type fits your job and where each falls short.
- The best cutting fluid for stainless steel matches the operation, tool, and delivery system—not just the metal.
- Evodyne cutting fluid is a Made-in-USA general-metal option; confirm stainless suitability before choosing it for stainless work.
- Choose stainless-rated neat cutting oil for localized drilling and tapping lubrication.
- Choose water-miscible coolant for compatible flood systems; cutting paste suits localized application.
Why this matters
Cutting fluid cannot rescue a tool that rubs instead of cuts. Stainless steel requires suitable tooling, appropriate cutting conditions, and effective lubrication at the cutting edge. Austenitic stainless grades such as 304 and 316 can work-harden when the tool rubs against the surface.
That makes fluid selection part of the setup, not a substitute for it. A bottle labeled for metalworking does not automatically establish suitability for every stainless grade, cutter, or machine.
For a 2026 purchase, separate 2 decisions: whether the formulation suits stainless steel and whether you can deliver it where cutting happens. A fluid that fits one decision but fails the other is the wrong choice.
What makes the best cutting fluid for stainless steel?
Use these criteria before comparing products. A specific application statement matters more than a broad claim about metal cutting.
- Material suitability: Look for explicit stainless-steel guidance. Identify your grade where possible; do not treat every stainless alloy as interchangeable.
- Operation fit: Drilling, tapping, milling, and turning create different demands. Choose a formulation intended for your operation rather than assuming universal coverage.
- Delivery method: Match the fluid to manual application, flood delivery, or another approved system. Never put an ordinary cutting oil into an atomizing system without checking suitability.
- Cooling and lubrication: Localized lubrication and sustained heat removal are different priorities. Select the balance your process needs.
- Cleanup and handling: Read the safety data sheet and directions for storage, exposure precautions, residues, and disposal. Cleaning requirements matter when the finished part has another use.
There are 4 checks before purchase: material, operation, delivery, and handling. Treat cleanup as part of handling, not something to discover after machining.
Cutting fluids at a glance
This 2026 comparison ranks application fit, not laboratory performance. The branded option has a stated general-metal purpose; the other entries are fluid categories whose individual formulations require checking.
| Option | Best for | Standout characteristic | Key limitation |
|---|---|---|---|
| Stainless-rated neat cutting oil | Localized drilling and tapping | Oil-based lubrication applied at the cutting point | Not the default for a machine requiring water-miscible flood coolant |
| Evo Dyne Cutting Fluid, Made in USA - Multipurpose Metal Cutting Oil | DIY general-metal work with a Made-in-USA preference | Multipurpose metal cutting oil with drilling, tapping, and milling named in the supplied product listing | Stainless-specific suitability is not established by the supplied product description |
| Water-miscible cutting coolant | Sustained cutting in a compatible flood system | Water-based coolant delivery after preparation according to its directions | Requires concentration control and system maintenance |
| Stainless-rated cutting paste | Localized application where a liquid runs away | Paste consistency helps keep the initial application in place | Does not replace continuous coolant delivery |
1. Stainless-rated neat cutting oil: best for drilling and tapping
A neat cutting oil is used without dilution unless its manufacturer directs otherwise. For manual drilling and tapping, choose a formulation explicitly intended for stainless steel and the operation you are performing.
The useful distinction is not simply oil versus water. It is whether the formulation provides appropriate lubrication at the tool’s working edge and whether your setup permits you to apply it effectively.
Stainless-rated neat cutting oil pros:
- Avoids the mixing step associated with water-miscible concentrates.
- Fits localized application on suitable manual jobs.
- Offers a direct selection route when the manufacturer names stainless drilling or tapping.
Stainless-rated neat cutting oil cons:
- Leaves an oily residue that requires appropriate cleanup.
- Does not automatically meet a machine’s cooling or circulation requirements.
- Requires attention to the formulation’s exposure precautions and compatibility guidance.
Do not select oil by thickness alone. Viscosity does not prove stainless suitability, and a heavy-looking liquid is not evidence of better tool protection.
For tapping, confirm that the oil suits the tap and workpiece. For drilling, apply it using a safe method that reaches the working area without bringing your hands near rotating equipment. Follow the tool maker’s cutting recommendations rather than copying settings from a different metal.
Best for: Localized stainless drilling and tapping where the tool and equipment permit neat-oil use.
Verdict: Buy a stainless-rated neat cutting oil for localized drilling and tapping; skip formulations without clear application guidance.
2. Evodyne cutting fluid: best for DIY general-metal maintenance
Evodyne’s cutting fluid is a Made-in-USA multipurpose metal cutting oil. Its supplied description identifies metal drilling, and its product listing names drilling, tapping, and milling applications.
Evodyne cutting fluid is best for DIY buyers seeking a Made-in-USA general-metal cutting oil, with stainless suitability confirmed before use. That is the useful buying distinction here—not an unsupported claim that it outperforms specialist stainless formulations.
Evodyne cutting fluid pros:
- Made-in-USA positioning is explicitly stated in the product information.
- General-metal cutting is the product’s stated purpose.
- Drilling, tapping, and milling appear in the supplied listing.
Evodyne cutting fluid cons:
- The supplied description does not explicitly establish stainless-grade compatibility.
- It does not establish dilution requirements or suitability for a particular coolant delivery system.
- No comparative stainless-machining results support a performance ranking against other formulations.
Choose this option by application, not by extrapolating from the word multipurpose. Before using it on stainless steel, read the current directions and confirm suitability for the alloy, cutting tool, and equipment.
That check is especially important if your project changes from manually drilling a bracket to running a machine with coolant circulation. Those are different fluid-selection decisions even when both involve metal cutting.
Best for: DIY general-metal work where a Made-in-USA product matters and the directions match the intended job.
Verdict: Hold for stainless-specific work until compatibility is confirmed; choose it for general-metal applications supported by its directions.
3. Water-miscible coolant: best for sustained flood-cooled machining
Water-miscible cutting coolants are prepared with water according to the formulation’s instructions. Depending on the product, this category includes soluble oils, semisynthetic fluids, and synthetic fluids.
For sustained milling or turning, the delivery system matters as much as the container label. A compatible flood setup moves coolant to the cutting zone and supports heat removal; it also requires an appropriate fluid-management routine.
Water-miscible coolant pros:
- Fits machines designed for compatible flood coolant.
- Supports cooling during sustained cutting.
- Provides a category of formulations with application-specific technical guidance.
Water-miscible coolant cons:
- Requires correct preparation and concentration checks.
- Needs attention to contamination and coolant condition.
- Is not a practical substitute for localized oil application when you lack a suitable delivery system.
Do not copy a mixing ratio from another coolant. Follow the selected manufacturer’s instructions, including mixing order, water-quality requirements, and monitoring method.
In 2026, choose the formulation and maintenance procedure together. A concentrate is not a complete solution if you have no way to check concentration or maintain the system.
Keep the selection tied to the machine manual and tool guidance. A coolant intended for one operation is not automatically appropriate for every stainless job, and an unsuitable fluid can create equipment or process problems.
Best for: Sustained stainless milling or turning on equipment designed for a compatible water-miscible flood coolant.
Verdict: Buy when your machine and stainless application call for it; skip for a simple manual job without suitable coolant delivery.
4. Stainless-rated cutting paste: best for localized starting points
A cutting paste has a thicker consistency than a free-flowing liquid. That makes it useful when you need the initial application to remain near a marked hole or another localized working point.
Select a paste whose directions explicitly cover stainless steel and your operation. Paste consistency alone says nothing about the formulation’s suitability for the alloy.
Stainless-rated cutting paste pros:
- Helps keep the initial application at a localized point.
- Suits some manually lubricated drilling and tapping operations.
- Avoids relying on a liquid that immediately runs off the application area.
Stainless-rated cutting paste cons:
- Does not provide continuous flood cooling.
- Requires safe reapplication according to the operation and directions.
- Leaves residue that needs appropriate removal.
Paste is a delivery choice, not a shortcut around tool selection. You still need a suitable cutting edge, secure workholding, and cutting conditions appropriate to the stainless grade.
Avoid reaching toward a rotating tool to replace material that has moved away. Stop and follow the equipment’s safe application procedure. If the operation requires uninterrupted coolant delivery, choose a compatible system rather than repeatedly applying paste by hand.
Best for: Localized stainless drilling or tapping where retaining the initial application matters and paste use is approved.
Verdict: Buy for suitable localized application; skip when the process requires continuous cooling or circulation.
How to choose and use the right fluid
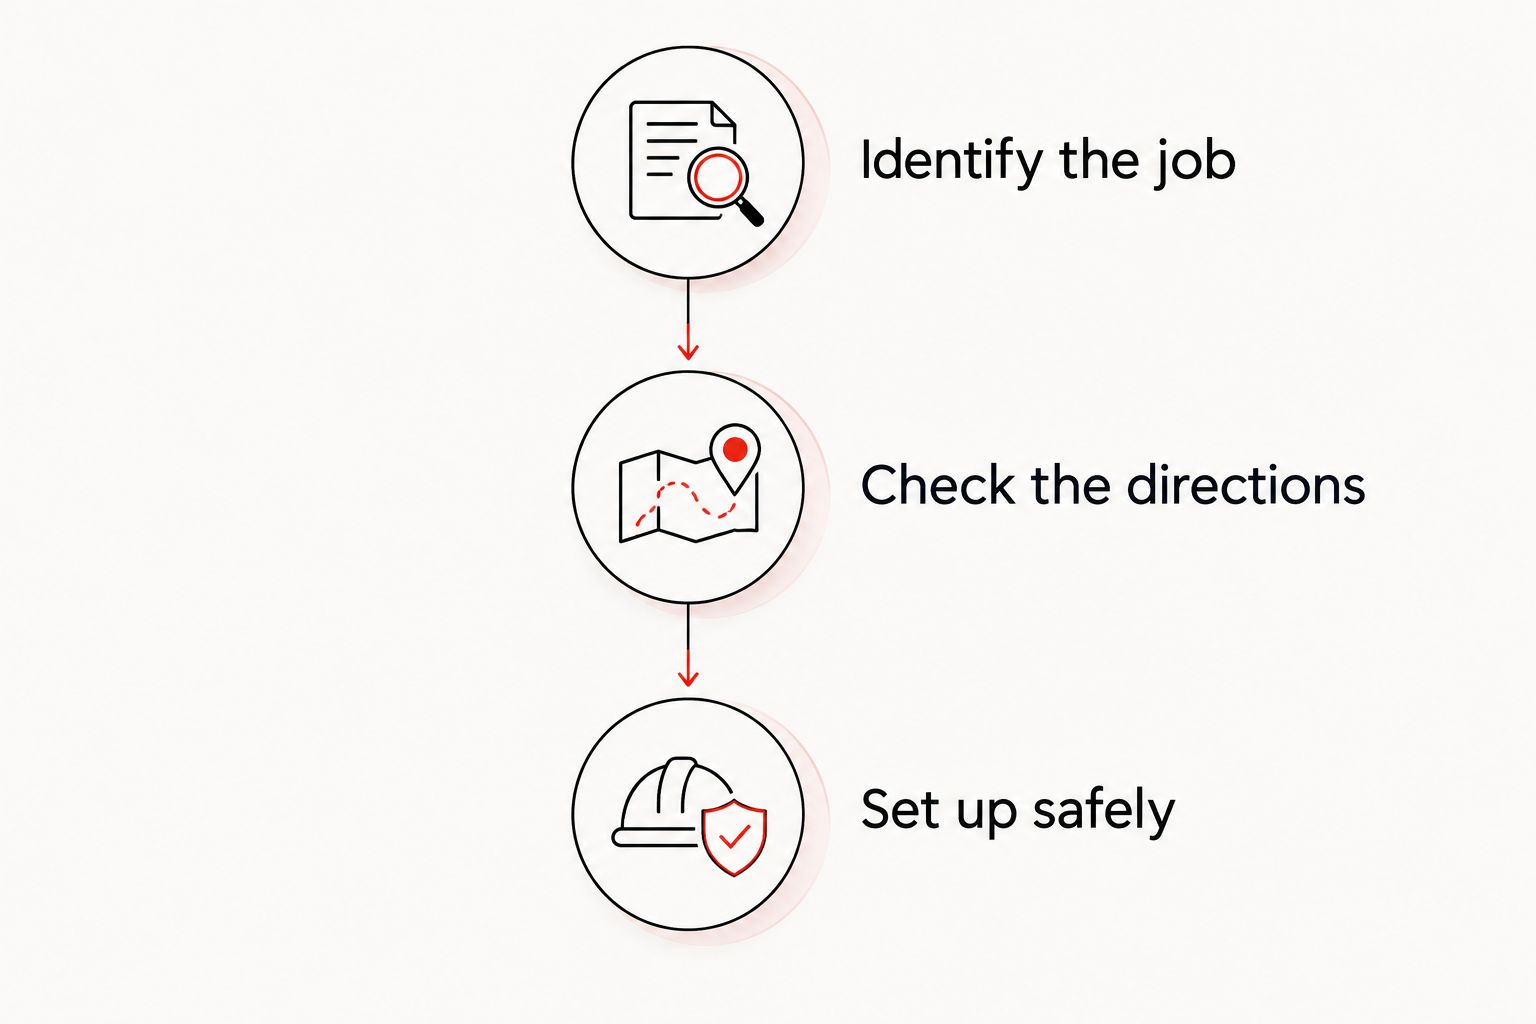
Use this 3-stage sequence for your 2026 setup. It keeps the purchase tied to the job rather than to a generic best-product label.
- Identify the job: Record the stainless grade if known, the operation, the cutting tool, and the machine or hand tool. Decide whether the job uses localized application or a coolant system.
- Check the directions: Read the fluid’s technical directions and safety data sheet. Confirm stainless suitability, preparation requirements, equipment compatibility, and handling precautions.
- Set up safely: Secure the workpiece, prepare the specified application method, and follow the tool maker’s cutting guidance. Stop if the tool rubs, the setup becomes unstable, or the application method is unsafe.
Keep 2 documents within reach: the product directions and the safety data sheet. Use the directions for application; use the safety data sheet for hazards, protective measures, storage, and disposal guidance.
Do not improvise a blend of household cleaners, penetrating oils, or different cutting fluids. A mixture has no established application guidance just because each ingredient has a familiar use.
Cleanup is part of the job. Follow the fluid’s instructions and the requirements of the finished component, particularly where residue would interfere with later coating, assembly, or use.
How these options are ranked
The ranking follows material suitability, operation fit, delivery, cooling and lubrication needs, and handling. It separates localized manual work from sustained machine cutting because those jobs do not share one default fluid.
This is an application-based buying guide, not a measured tool-life comparison. No cutting-speed gains, finish improvements, or comparative wear results are claimed for the listed options.
Which cutting fluid should you choose?
For an undecided DIY reader drilling or tapping stainless, start with a stainless-rated neat cutting oil approved for the operation. It is the clearest default when localized application fits the equipment.
Choose water-miscible coolant when your machine requires a compatible flood system. Choose stainless-rated paste when retaining a localized application is the priority. Keep the branded general-metal option conditional on explicit stainless guidance.
The best 2026 choice is the one whose directions match your actual setup. Do not buy a different delivery format merely because it ranks higher for someone else’s operation.
FAQ
What's the best cutting fluid for stainless steel?
A stainless-rated neat cutting oil is the default for localized drilling and tapping; a compatible water-miscible coolant fits sustained flood-cooled machining. Match the formulation to your tool, alloy, and delivery system.
Is Evodyne cutting fluid suitable for stainless steel?
The supplied product information establishes general-metal cutting applications, not stainless-specific compatibility. Confirm the current directions cover your stainless grade and operation before using it.
Is cutting oil better than water-based coolant for stainless?
Cutting oil fits localized lubrication, while water-miscible coolant fits compatible systems that need sustained cooling. Neither category is universally better; the operation and machine determine the choice.
Can I use cutting paste for drilling stainless steel?
Use cutting paste when its directions cover stainless drilling and your tool permits that application method. Paste helps retain the initial application but does not replace continuous coolant delivery.
Should I dilute cutting oil before using it?
Dilute a cutting fluid only when its manufacturer instructs you to. Neat oils and water-miscible concentrates are different categories, and their preparation instructions are not interchangeable.
Why does my drill stop cutting stainless even with lubricant?
Lubricant does not correct unsuitable tooling or a cutting edge that is rubbing rather than cutting. Stainless can work-harden, so stop and check the tool, workholding, cutting conditions, and fluid delivery.
What should I check before buying stainless cutting fluid in 2026?
Check material suitability, operation fit, delivery method, and handling requirements. Read the product directions and safety data sheet, then compare them with the machine and tool guidance.
One last thing
Do not treat stainless compatibility as an ingredient you can add later. If the application guidance does not establish the match, a thicker coating or another fluid mixed in does not establish it either.
Write down the operation before shopping. A clear description of the job is more useful than a longer list of bottles.